ISA-95 Integration Without an MES
The Layer Nobody Bought
Most Australian plants have a control system at the bottom and an ERP at the top, and almost nothing deliberate in between. The SCADA or DCS runs the process. SAP, Pronto, MYOB Advanced or Microsoft Dynamics runs the business. Between them sits a gap that was supposed to be filled by a Manufacturing Execution System, and in a great many sites that MES was never bought, never finished, or quietly died after the one person who understood it left.
The gap does not announce itself. It shows up as a production number that finance types into a spreadsheet off a printout, a quality result that lives in a lab database no other system can read, and a maintenance backlog that nobody can line up against the asset register in the ERP. Everyone assumes there is a system doing this work. There is a person doing it, by hand, at month end.
This article is for plant managers, operations leaders and the finance and IT people who keep asking why the factory cannot give them a clean number without a three day scramble. The reference model that makes the gap legible, and gives you a defensible way to close it without a multi-year MES programme, is ISA-95. Having worked on enterprise-to-plant data systems for BHP, Rio Tinto and Senex Energy while employed by previous consulting and engineering firms, across an 18 year career in industrial data, I can tell you the sites that struggle are rarely short of systems. They are short of the one integration layer that nobody put a purchase order against.
What ISA-95 Actually Is
ISA-95 is the ANSI/ISA-95 Enterprise-Control System Integration standard, published internationally as IEC 62264. It is not a product and not something you install. It is a shared model of how a manufacturing or processing business is layered, from the physical process at the bottom to the business systems at the top, and a common vocabulary for the information that has to move between those layers.
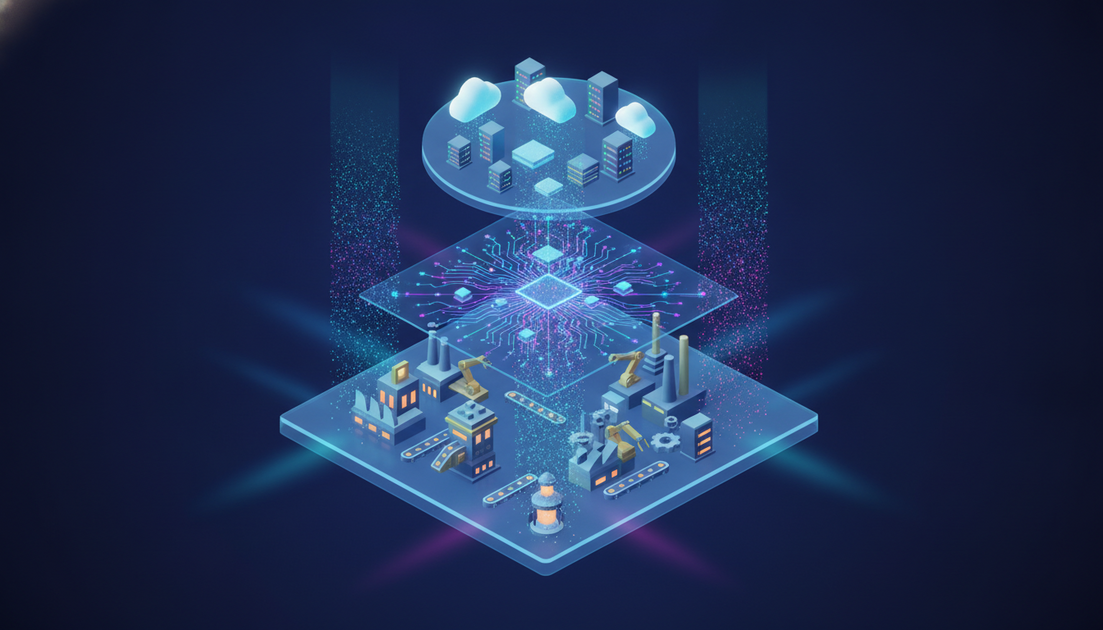
The model describes five levels. Level 0 is the physical process, the valves, motors and material itself. Level 1 is the sensing and actuation, the instruments and final control elements. Level 2 is the monitoring and control, the SCADA, PLCs and DCS that run the plant in real time. Level 3 is manufacturing operations management, the scheduling, dispatching, quality, maintenance and performance work that an MES is built to do. Level 4 is the business, the ERP and the planning and financial systems that run the enterprise.
The reason the model matters to a site with no MES is simple. Level 3 is exactly the layer you are missing. The value of ISA-95 is not that it tells you to buy an MES. It is that it gives you a precise way to describe which Level 3 functions your business actually needs, so you can build or integrate only those, rather than being sold a platform that does forty things when you need six.
The ISA-95 Levels and Where the Gap Sits
The standard also describes the information that crosses the Level 3 to Level 4 boundary: production schedules going down, production performance coming back up, plus definitions of products, resources and capability. This is the part people skip. They argue about which MES product to buy before they have written down what information actually needs to move, in what shape, and how often. ISA-95 Part 3 gives you the activity model to do that first, and that work is useful whether you end up buying a product, building a small integration, or doing something in between.
Why the Gap Persists
The MES-sized hole in the middle of a plant is almost never the result of a single bad decision. It accumulates. A site commissions a control system from one vendor and an ERP from another, years apart, each chosen by a different part of the business for a different reason. The control system vendor assumes the business will buy their MES module. The ERP vendor assumes the plant will feed it clean data. Neither assumption holds, and the integration that was supposed to be somebody's job becomes nobody's job.
Then the spreadsheets arrive. They are fast, they work, and they are invisible to anyone making a technology decision. A production accountant builds a workbook that pulls numbers off the historian and reconciles them to the ERP. It becomes load bearing. By the time anyone notices, the business is running its most important operational figures through a file on one person's laptop, and that person is a single point of failure sitting on top of the number the board trusts.
Buying an MES vs Closing the Gap with ISA-95
| Metric | Full MES programme | Targeted ISA-95 integration | Improvement |
|---|---|---|---|
| Scope | Vendor platform covering all Level 3 functions | Only the Level 3 functions the business needs | Scoped |
| Timeline | 12 to 36 months, often stalled | Delivered in phases, first value in weeks | Phased |
| Dependency | Locked to one vendor's roadmap and licensing | Standards-based interfaces you can maintain | Portable |
| Risk | Big-bang cutover, high failure rate | Incremental, each piece validated before the next | Lower |
None of this is an argument against buying an MES. Large, complex sites with genuine Level 3 needs across scheduling, genealogy, quality and maintenance may be right to buy one. The argument is against buying one by reflex, before the business has used the ISA-95 model to work out which functions it actually requires. Most sites that think they need a full MES need three or four of its functions and a clean set of interfaces.
Mapping Your Own Site to the Model
The first piece of real work is a mapping exercise, and it is cheaper and more useful than any software evaluation. You take each level of the model and write down, honestly, what system fills it today and what information crosses each boundary.
At Level 2 you list every control system and historian, with its tags, its scan rates and its real owner. At Level 4 you list the ERP modules that touch production: inventory, costing, maintenance, planning. Then you look at Level 3 and write down what is there. On most sites the honest answer is a mix of spreadsheets, a lab information system that talks to nothing, a maintenance module in the ERP that nobody updates from the floor, and a scheduling whiteboard.
The gap becomes a list. Each item on the list is a specific Level 3 function and a specific data exchange that is being done by hand or not at all. That list is the brief. It is also, when you cost the manual effort and the error exposure against it, the business case.
What Does Your Site Actually Need at Level 3?
The discipline of the model is that it forces you to name the specific exchange rather than the general ambition. "We need better visibility" is not a brief. "The historian needs to send a validated, reconciled daily production total to the ERP in this shape by 6am" is a brief. You can build the second one. You can test it. You can prove it works before you spend a dollar on the next piece. The problem of production numbers that disagree across SCADA, the historian and the ERP is almost always a missing or badly defined Level 3 to Level 4 exchange, and the model tells you exactly where to put the fix.
Building the Integration, Not the Monolith
Once you have the list, the integration gets built in the order that the business feels most, one exchange at a time. This is where the standard earns its keep, because ISA-95 defines the shape of the common exchanges. You are not inventing a data contract from nothing. You are implementing a well-described one.
A production reporting interface takes the historian's time-series data, applies the same reconciliation logic every time, and delivers a single defensible number to the ERP on a schedule. A quality interface takes lab results and attaches them to the production record so a batch can be released or held without anyone rekeying a certificate. A maintenance interface takes condition data off the plant and raises or closes work in the ERP against the real asset.
Each of these is a small, testable piece of software with a defined input, a defined output and a defined owner. None of them requires ripping out a working control system. This is the same principle covered in our guide to connecting modern tools to legacy systems without a rip and replace: you wrap and interface what works, you do not replace it to satisfy an architecture diagram.
A Phased ISA-95 Integration
The phased approach has a second benefit that matters to anyone who has watched a big industrial IT project stall. Every phase ships something that works. There is no distant go-live where all the value arrives at once, or does not. If the budget pauses after phase one, you still have a working production reporting interface and you are better off than you were. Industrial analytics projects fail far more often from scope and sequencing than from technology, and a phased, exchange-by-exchange build is the direct answer to that failure mode.
Where AI and Analytics Fit, and Where They Do Not
It is tempting to jump straight to the analytics. Everyone wants the dashboard, the forecast, the anomaly alert. The uncomfortable truth is that none of that works on a plant with no Level 3 layer, because the data arriving at Level 4 is unreliable, late and inconsistent. An agent or a model built on that foundation produces confident answers off bad numbers, which is worse than no answer at all.
ISA-95 is, in effect, the data foundation that analytics and AI need. Once the Level 3 to Level 4 exchanges are clean and defined, the reporting that used to take a three day manual scramble becomes a query, and the historian data that was trapped at Level 2 becomes available to report on in Power BI without building a second historian. Only then does it make sense to layer analytics or an agent on top. We make this argument in full in our piece on why agentic AI needs a real data foundation: the model is not the hard part, the plumbing underneath it is.
What the Integration Returns
For businesses running a central control room or consolidating several sites, the same discipline underpins what a remote operations centre actually needs. You cannot run operations from a distance on data you do not trust, and the trust comes from the defined exchanges, not from the size of the screens on the wall.
The Governance Question for the Board
There is a board-level dimension to all of this that operations leaders often leave unsaid. The most important operating number a manufacturing or processing business produces, how much it made and whether that reconciles to what it sold, is in many Australian businesses dependent on an undocumented spreadsheet maintained by one person. That is an operational risk, a reporting risk and an audit risk sitting in plain sight.
Framing the ISA-95 integration as risk reduction, rather than as an IT upgrade, changes who pays attention to it. A board that would not fund a vague MES project will fund the removal of a single point of failure on its production reporting once the exposure is named. This is the same conversation we set out for directors in our guide to AI advisory for Australian boards: the question is not which technology to buy, it is which risk the business is carrying because the integration layer was never built.
How to Start
You do not start by evaluating MES vendors. You start by mapping your own site against the five levels and writing down every exchange that is currently done by hand or not at all. That document, with the manual effort and error exposure costed against each item, is both your brief and your business case. From there, the build is phased, standards-based and testable, and it can stop at any phase with value already banked.
Solve8 works with Australian manufacturers and processing operations to map a site against ISA-95, name the exchanges that matter, and build the integration layer in phases rather than as one high-risk programme. If your plant has SCADA, a historian and an ERP but nothing reliable in between, the first step is a scoping conversation about what your Level 3 actually needs to do. We look at your systems, your reconciliation pain and your reporting deadlines, and we tell you honestly whether you need a handful of interfaces or a genuine MES. You can see the broader way we approach enterprise AI and system integration work across asset-heavy Australian operations, or get in touch to scope the gap in your own plant.